
Tool breakage is an occasional reality in machining, even in well-managed production environments. A broken drill, tap, or other cutting tool can interrupt a job and place the workpiece at risk. When the fragment becomes trapped inside a hole, removing it without damaging the component can require careful planning and specialised equipment.
Electrical discharge machining is one approach used for certain broken-tool recovery situations, particularly where the fragment is conductive and conventional cutting methods are unsuitable.
Understanding the Consequences of a Broken Tap
A tap creates internal threads in a prepared hole. If it breaks during operation, the remaining piece may be lodged firmly in the workpiece. Hardened tool material can be difficult to machine, and attempts to remove it with excessive force may damage the threads or surrounding material.
The consequences extend beyond the immediate repair. A delayed component may hold up an assembly, disrupt a production schedule, or require costly replacement if recovery fails.
The first step is to stop the operation and assess the situation. Identify the broken tool, the workpiece material, the fragment’s position, and the value and precision requirements of the component.
How Electrical Discharge Machining Helps
EDM removes conductive material through controlled electrical discharges. Unlike conventional drilling, it does not depend on a cutting edge mechanically shearing the material.
For selected broken-tool recovery tasks, an appropriate electrode can be used to erode the trapped fragment. The aim is to remove enough material to facilitate extraction while controlling the effect on the surrounding workpiece.
The result depends on the equipment, electrode, fragment geometry, material properties, and operator setup. EDM should therefore be selected only after confirming that the method is suitable for the particular case.
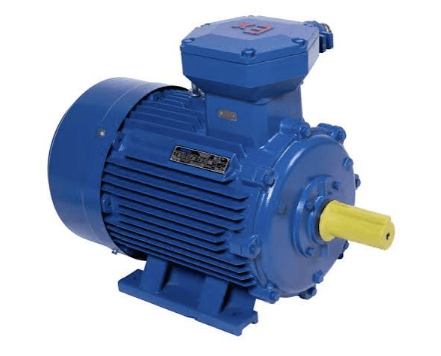
For businesses researching this category, the Clyertek EDM broken tap remover provides a product reference for evaluating equipment designed for selected broken-tool removal applications.
Evaluating Whether Recovery Is Feasible
Identify the materials
EDM generally requires an electrically conductive workpiece and a suitable electrode-to-material interaction. Confirm the material of both the broken tool and the component before selecting a procedure.
Unknown materials, coatings, or unusual alloys may require further assessment. Material identification helps prevent unsuitable operating assumptions.
Assess fragment location and access
The position of the broken tap influences the available setup and removal strategy. A fragment close to the surface may present different challenges from one located deep within a narrow hole.
Determine whether the workpiece can be secured and whether the electrode can reach the required area. Nearby features may need protection, and some parts may require specialised fixtures.
Establish the required final condition
Removing the fragment is only part of the task. The original hole may need to retain its dimensions and thread quality, especially when it is part of a precision assembly.
Define the inspection requirements before starting. Depending on the component, the recovered hole may require cleaning, dimensional checks, thread inspection, or further machining.
Comparing Recovery Methods
Several approaches may be considered when a tap breaks. Conventional extraction techniques may work in suitable cases, while other methods may be appropriate when the fragment is accessible and the workpiece can tolerate the process.
EDM can be worth investigating when a hardened conductive fragment is difficult to machine conventionally. However, the best method depends on the actual case, and no approach guarantees successful recovery.
Compare the options by considering the probability of preserving the component, the time required, equipment availability, operator skill, and the cost of potential damage. For expensive parts, obtaining advice from an experienced technician may be more economical than attempting repeated extraction methods.
Carrying Out a Controlled Recovery Process
A reliable procedure begins with a secure workpiece and a verified setup. Operators should follow the equipment manufacturer’s instructions and use approved settings and accessories.
During processing, monitor the operation according to the prescribed procedure. Avoid excessive force, improvised electrode arrangements, or unapproved changes to the equipment.
After the fragment is removed, clean and inspect the hole. Check for remaining material, damaged threads, and changes that could affect the component’s function. The appropriate inspection method depends on the part’s tolerances and service requirements.
For safety-critical or precision components, a qualified person should approve the recovery result before the part returns to service.
Improving Production Practices to Prevent Breakage
Recovery equipment addresses the consequences of tool failure, but prevention remains important. Review whether the correct tap was selected for the material and thread specification. Check tool wear, alignment, cutting speed, lubrication, and chip evacuation.
Ensure that the drilled hole meets the required dimensions before tapping. Poor preparation can increase cutting resistance and raise the risk of breakage.
Operators should be trained to recognise abnormal torque, vibration, or other signs that the process may be going wrong. Preventive maintenance and consistent machining procedures can reduce the frequency of avoidable failures.
Evaluating the Financial Impact
A recovery decision should include more than the equipment’s purchase price. Consider labour, setup, production downtime, consumables, inspection, and the value of the component being recovered.
Businesses that encounter broken taps regularly may benefit from documenting the frequency, causes, and outcomes of recovery jobs. These records can reveal whether improved tooling practices, operator training, or dedicated recovery equipment would provide the greatest benefit.
Frequently Asked Questions
1. When should a workshop consider EDM for broken-tap removal?
It may be worth considering when a conductive fragment is difficult to remove mechanically and preserving the workpiece is important. Suitability must be assessed for each case.
2. Can the process damage the original hole?
Yes, inappropriate setup or operating conditions can affect the workpiece. Use an approved procedure and inspect the hole and threads after recovery.
3. How can machining teams reduce broken-tap incidents?
Review tool selection, alignment, hole preparation, lubrication, chip evacuation, tool condition, and cutting parameters. Operator training can also help identify problems early.
Conclusion
Broken-tool recovery requires a careful balance between removing the obstruction and preserving the value of the workpiece. EDM can provide an option for certain conductive fragments that are difficult to remove through conventional methods. Material assessment, a controlled procedure, and post-recovery inspection are essential. By combining appropriate recovery techniques with preventive machining practices, businesses can reduce unnecessary scrap and limit the disruption caused by tool failure.